
Advanced Hydraulic Slitting Line with Precision Tension Control for Steel Coils
The steel coil shear unit is mainly used for slitting of ordinary carbon coil and hot dip galvanizing and preparing blank for the next step.
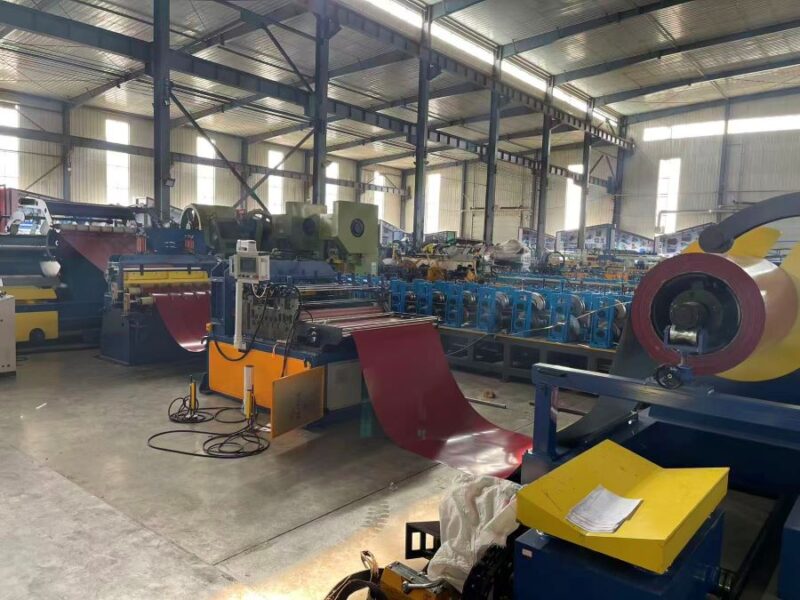
Composed device
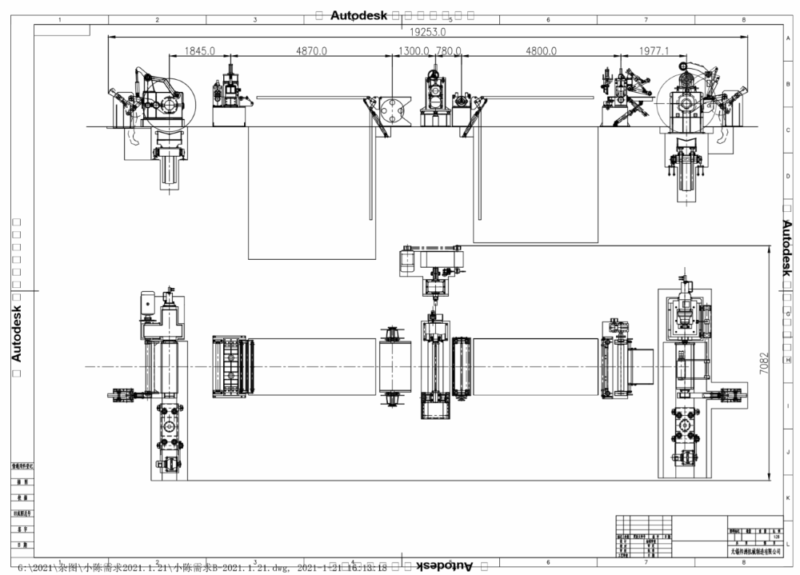
From right to left are: Entry coil car→Decoiler →Press and pinch device→Hydraulic cutter→Looper 1→Side guide device → Slitter →Scrap winder → Looper 2 →Tension stand →Recoielr →Exit coil car
- Entry Coil Car: 1 set
- Hydraulic Decoiler: 1 set
- Hydraulic Press and Pinch Device: 1 set
- Hydraulic Cutter: 1 set
- Looper I: 1 set
- Side Guide Device: 1 set
- Slitter: 1 set
- Scrap Winder: 1 set
- Looper II: 1 set
- Tension Stand: 1 set
- Recoiler: 1 set
- Exit Coil Car: 1 set
- Hydraulic System: 1 set
- Electrical System: 1 set
Main technical parameters
teel Coil Parameters
- Material: CRS and GI
- Tensile Strength: δb≤450Mpa, δS≤260Mpa
- Steel Thickness: 0.3-3.5mm
- Steel Width: 500-1600mm
- Steel Coil I.D: φ480-520 mm
- Steel Coil O.D: φ1600mm (max)
- Steel Coil Weight: 15T (max)
Slitter Parameters
- Knife Pivot Diameter: Ф220 mm
- Knife Pivot Material: 40Cr
- Blades Specification: Φ220mm X φ340mm X 15mm
- Blade Material: H13K
Slit Parameters
- Max Slit Quantity: 5 pcs (3-3.5mm) 8 pcs (2mm) 15 pcs (1mm) 25 pcs (0.3mm)
- Width Precision: ≤±0.05mm
Other Parameters
- Power: 380V/60Hz/3Ph
- Line Speed: 0-60m/min
- Capacity: Around 220 Kw
- Whole Line Dimension: 23m (L) X 8m (W)
- Daily Production Capacity: Around 40T (for 8 hours)
- Operator Needed: 1 mechanical engineer, 2 common workers
- Line Direction: From right to left (Face to machine)
Component Introduction
1.Hydraulic Entry Coil Car
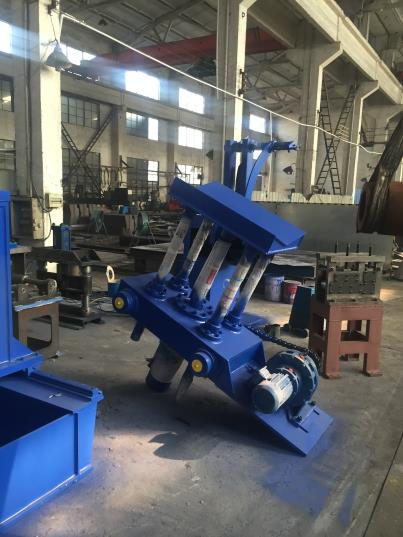
◆The car can move levelly and vertically, which is convenient for putting the steel coils into the de-coiler.
◆It is driven vertically by φ180mm hydraulic cylinder with 4 guide pillars
◆The level movement is driven by XWD2.2-63-121 cycloid motor
◆Capacity: 15T
◆Function: It is used to lift up and down, move forward and back to make it easy to load the coils on decoiler. Hydraulic controls lifting, motor drives moving. The car is controlled on the auxiliary control panel. Its moving speed is 6-7m/min. When the coils on decoiler, the car will return back to the start position. It can also carry back the unfinished coils from decoiler.
2.Hydraulic Decoiler
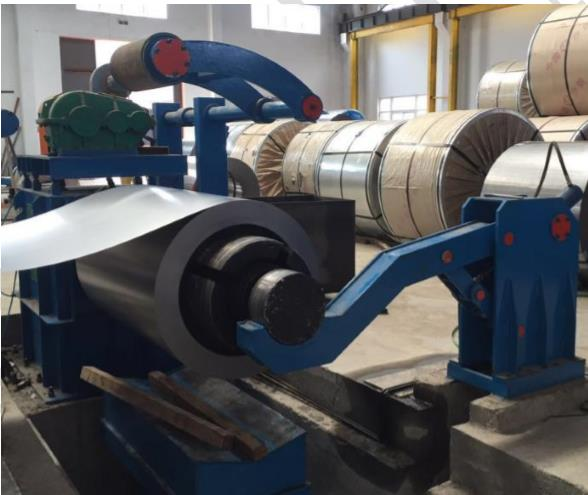
◆4KW motor drives the decoiler running and the hydraulic drives it expand and shrink.
◆Expanding model: oblique slider is driven by hydraulic oil cylinder.
◆Max loading weight: 15T
◆Mandrel:45# steel processed by heat treatment and the diameter is φ219mm. It is home-made by our company.
◆It is designed with the supporting stand which is driven by hydraulic to ensure the heavy weight of coils can be loading.
◆It is designed with the press arm, the roller is made by rubber, this design is used to prevent the coils from loosing.
3.Hydraulic Press and Pinch Device
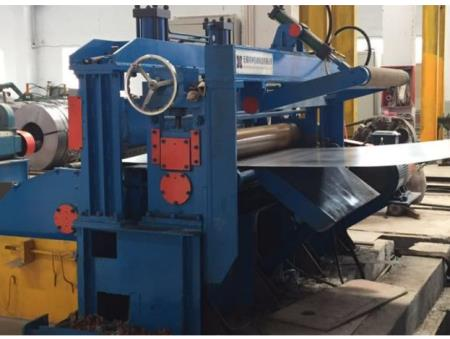
◆ Two hydraulic cylinders controlled unwinding rubber roller lifting.
◆ Hydraulic shovel head, hydraulic power shovel-head ect feeding steel plates.
◆ Hydraulic pressing & guiding device: Driven by 11KW cycloid reducer motor. Setting manual clutch. Pinch roller pressed by hydraulic cylinders.Drive mode using the lower roller drive. The diameter of hydraulic cylinder is: φ100
◆ Structure: It is welding by steel plates and profiled bar.
4.Hydraulic Cutter
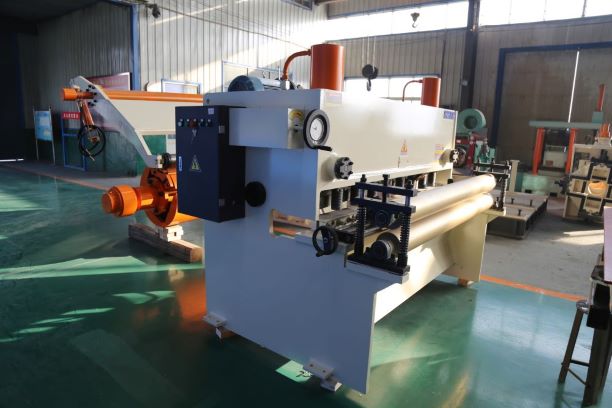
◆Adopt two columns structures, a press device, can cut the 3.5X1600mm steel plates ;
◆The up and down blades which are alloy material H13K can adjust their gap;
◆The machine is used for the steel shear and to make the plate easy to slitting machine.
5.Looper I
◆ The pit is equipped with 2 groups of magic eyes to control the speed buffer between decoiler and slitter
◆ The pit size: 4500mmX2000mmX3000mm.
6.Side Guide Device
◆It is composed of the frame, guide roller, adjustment device, movable platform and multi-roller wheel
◆ The vertical rollerson the both sides guide the sheet right into the slitter.
◆ Both sides of guiding vertical rollers adjust by the motor drives the both ends of the screw. The adjusting width is: 500-1600mm.
7.Slitter
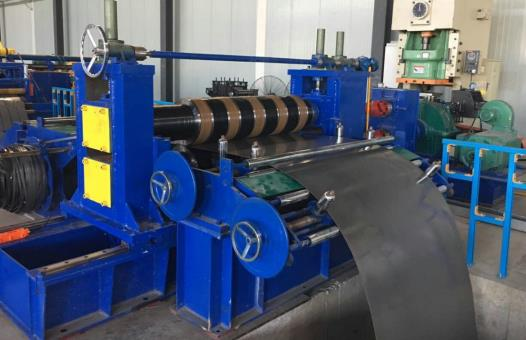
◆ Specification of blades:Φ340×Φ220×15 material:H13K .
◆Electric motor:75KW frequency conversion control motor to control the speed. Control mode is frequency control.
◆Reducer: cycloidal reducer
◆Function: It equips the side guide device, to achieve positioning strip and stop the jumping of strip. Improve the accuracy of slitting. It can shear actively orpassively. To achieve different strip thickness accuracy requirements of slitting.
8.Scrap Winder
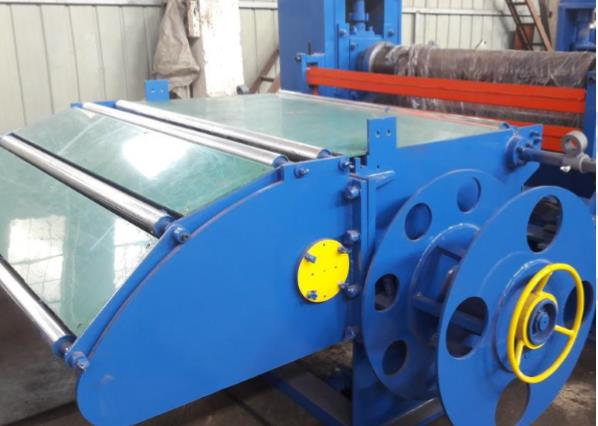
◆ It used to wind the scarp strips.
◆ It consists of base, the shaft and plate of scrap material, friction wheel, supporting wheel chain, chain, decelerator and 4Kw motor.
9.Looper Ⅱ
◆ The roller-table lift up and down by hydraulic.
◆The size of the pit: 4000mm(L)x2000mm(W)x5000mm(D)
10.Tension Stand
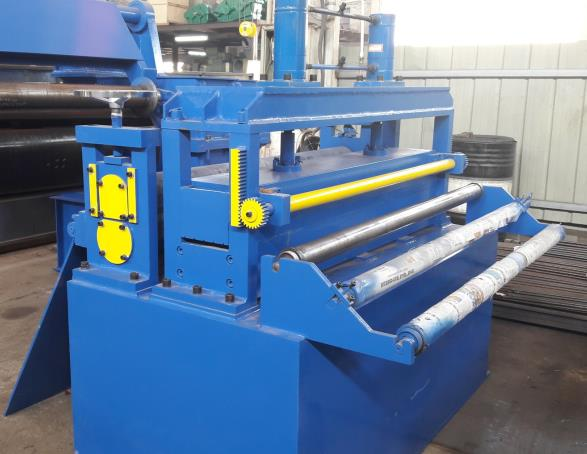
◆The frame welded by steel plates.
◆ Consist of base ,pre-dividing shaft, bracket, press shaft, hydraulic damp device and hydraulic shaft lifting the press down device. Supporting slices, spacers and etc.
◆ Function: It also have the side guide device for finished strips and prevent them from jumping and improve the recoiler quality. To establishing a stretching force with recoilier, to make sure the even quality and tight of steel coils after recoiling.
11.Recoiler
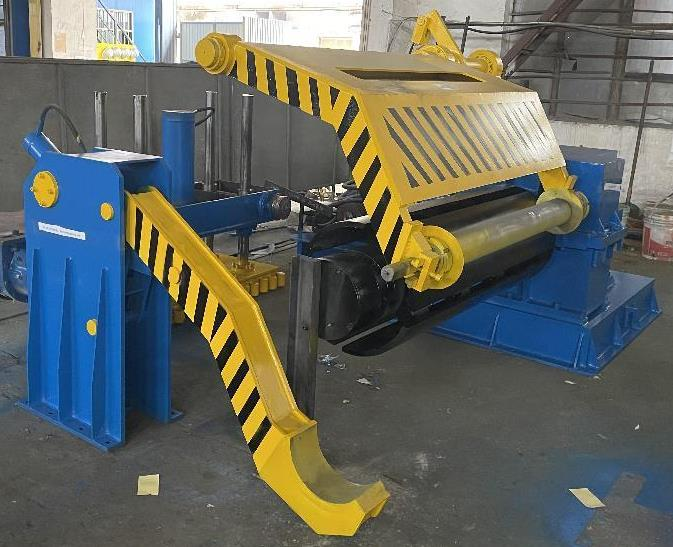
◆ tructure:hydraulic expand and shrink model.
◆ Specification of shaft: Φ508x1600mm;
◆Capacity:P≤15T with hydraulic supporting arm
◆ Motor:110KW AC
◆ Decelerator:JZQ650 i=40.17
◆ Overall steel plate cantilever structure
◆Function: It cooperates with the finished steel strips after first pre-dividing and second dividing to insure the even and tight quality of recoiler. Recoiling tension adjustable, Recoiling speed adjustable.
12.Hydraulic exit coil car
◆ The car can move levelly and vertically, which is convenient for putting the steel coils into the de-coiler.
◆ It is driven vertically by hydraulic cylinder with four guide pillars.
◆ The level movement is driven by cycloid motor.
◆The capacity of it can reach to 15tons(MAX)
13.Hydraulic system
◆ Composed of hydraulic oil pump, pipes, connectors, etc
◆ Ensure the use of every hydraulic part.
14.Electrical control system
◆It controls the speed of the whole line. The main operation table can make the whole line change from high to low speed. And it can also make the plate into the machine manually.